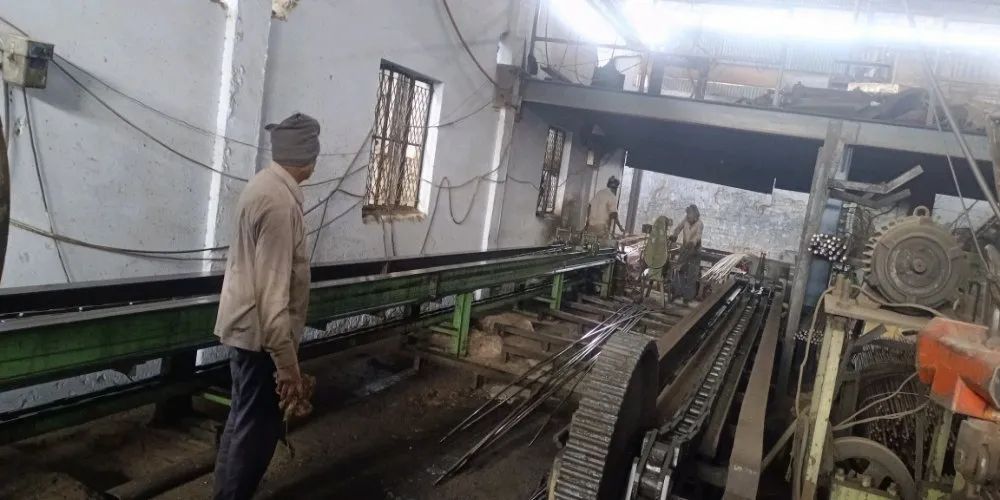
Manufacturing at our Ghaziabad works
Two production lines run under one roof: wire drawing for MS wire, and cold drawing for bright bars. Both start from hot rolled steel and finish at the exact size you order.
Wire drawing line
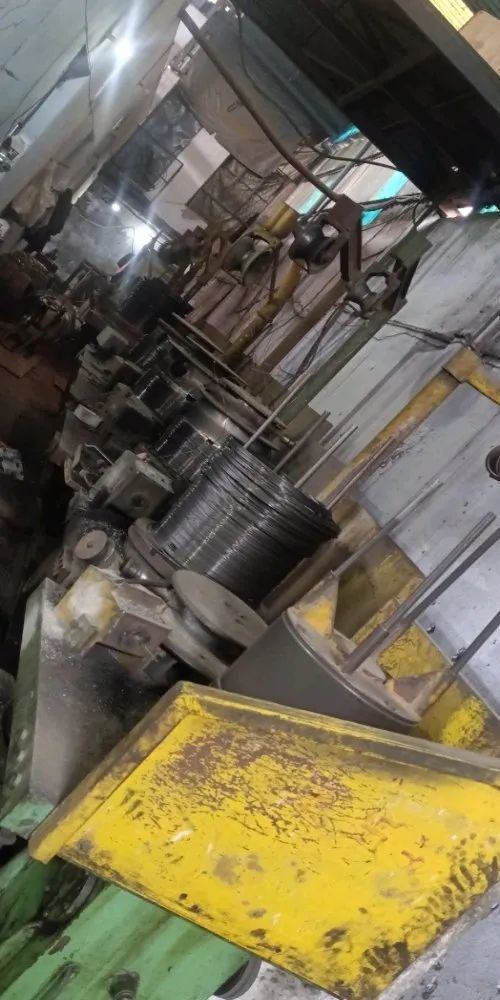
Drawing pulls hot rolled wire rod through a series of tungsten carbide dies, each slightly smaller than the last. The steel gets thinner, longer, stronger and smoother with every pass. The number of passes decides the final gauge and how hard the wire is.
Rod inspection
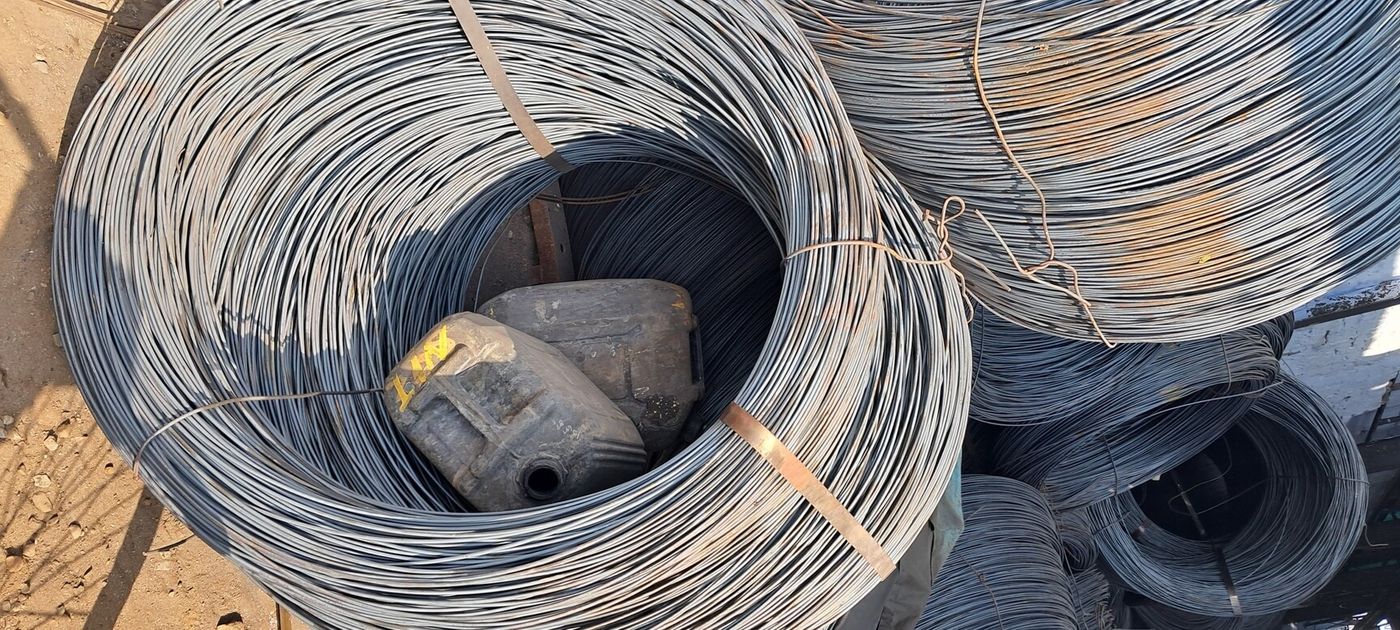
Incoming 5.5 mm to 8 mm wire rod coils are checked against the mill's test certificate for grade and diameter.
Descaling
The mill scale left by hot rolling is removed so that it does not score the dies or the wire surface.
Drawing
The rod runs through the die sequence on our drawing blocks until it reaches the ordered gauge. Diameter is checked with a micrometer at the start of every coil.
Annealing or galvanising, when ordered
Annealed wire is softened for tying and binding work. Galvanised wire gets a zinc coat for outdoor use and fencing.
Coiling and tagging
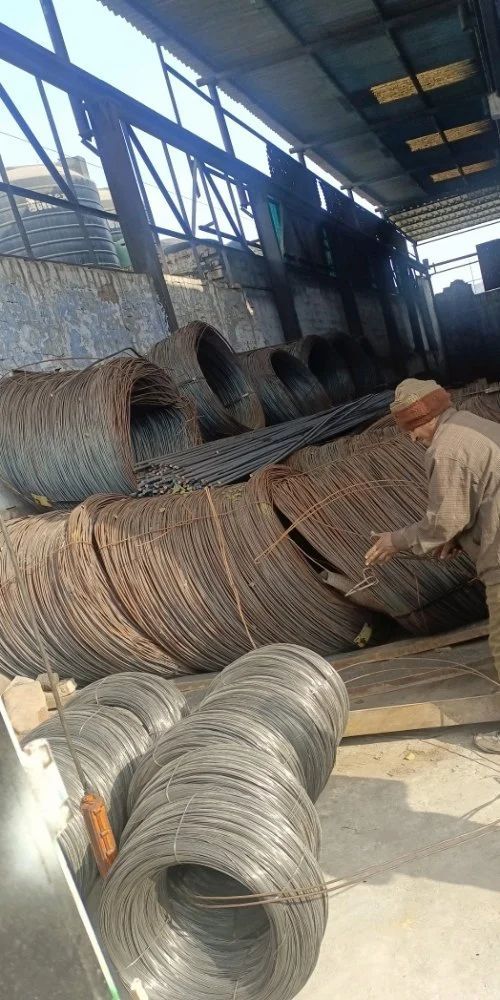
Finished wire is wound into coils, strapped and tagged with size, grade and weight for dispatch.
Bright bar line
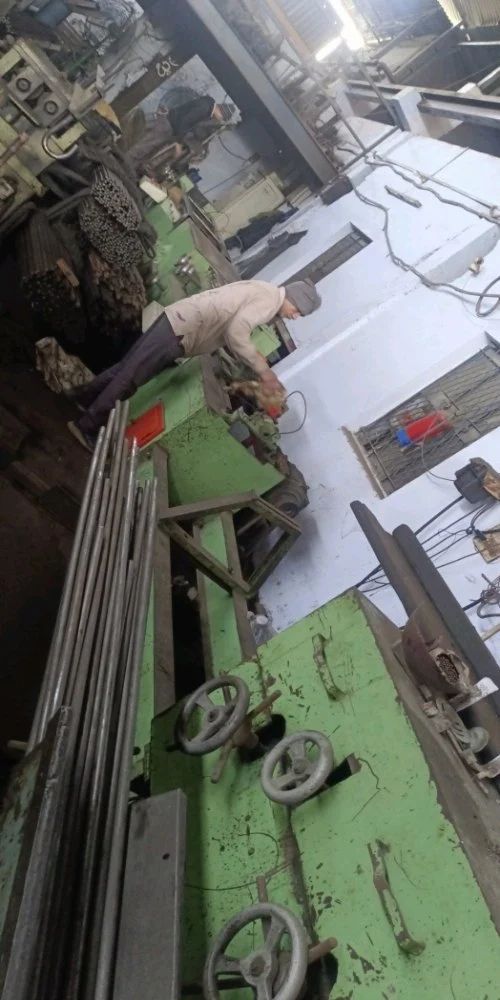
Bright bars are hot rolled bars that have been cold finished to a tight size and a clean, smooth surface. They machine better and look better than black bar, which is why they go into shafts, pins, fasteners and machined parts.
Pointing
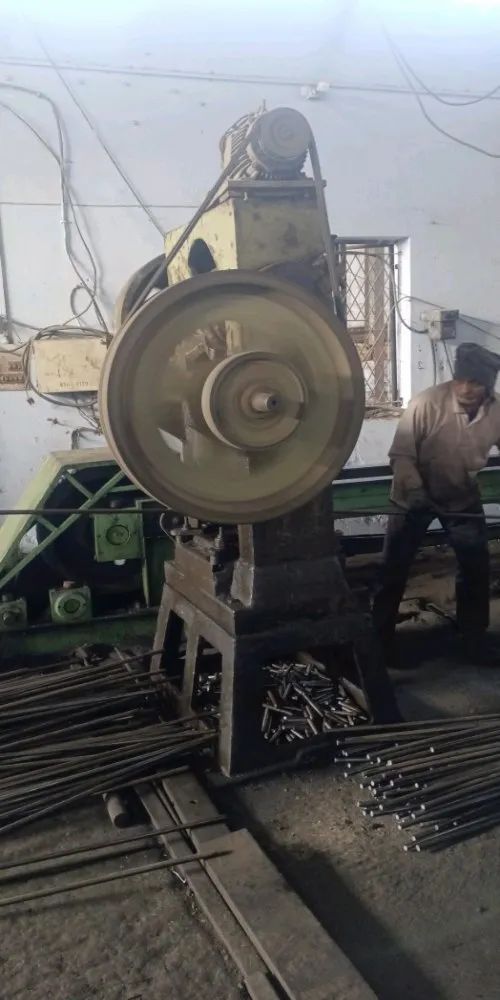
The end of each hot rolled bar is reduced so that it can enter the die.
Cold drawing
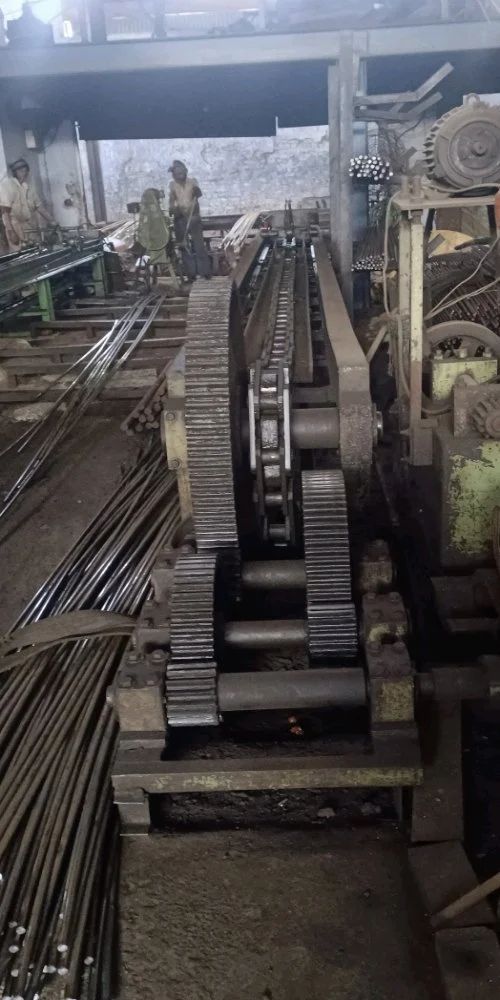
Our chain draw benches pull the bar through a round, hexagonal or square die, sizing it and work hardening the surface.
Peeling or grinding, when ordered
For closer tolerances and a finer finish, bars are peeled or ground after drawing.
Straightening and cutting
Bars are straightened and cut to standard 3 m or 6 m lengths, or to the length on your order.
What the works can produce
Typical ranges. Other sizes and grades can often be made to order, so ask before ruling us out.
| Product | Size range | Grades and standards | Finish |
|---|---|---|---|
| MS wire rod coils | 5.5 mm to 12 mm | SAE 1008, SAE 1010 | Black (as rolled) |
| HB (hard bright) wire | 4.88 mm to 1.22 mm (6 to 18 SWG) | Low carbon mild steel | Bright drawn |
| Galvanised (GI) wire | 4 mm to 1.22 mm | Low carbon mild steel | Hot dip galvanised |
| Round bright bars | 6 mm to 100 mm | EN1A, EN8, IS 2062 E250 | Cold drawn, peeled, ground |
| Hexagonal bright bars | 6 mm to 20 mm A/F | EN1A, EN8 | Cold drawn |
| Square bright bars | 10 mm to 16 mm | EN8, IS 2062 | Cold drawn |
Tolerance classes h9 and h6 are available on bright bars. Mill test certificates are supplied on request.
Need a size that is not listed?
Send us the gauge or diameter, grade, finish and quantity. If our lines can draw it, we will quote it.